Explore our precision-engineered sports gear, specialized accessories, and industrial safety netting built for ultimate durability.

Our Sales Team have strong sourcing ability and professional work ethics. We provide more than prompt, professional service.

We understand that the bottom line matters. That's why we offer valuable extras such as free design and free existing samples to meet your needs.

We realize the shipping & package are important to customers. So we cooperate with the most competitive logistics company whom have agreement with carrier directly.

When you partner with us, you will know that your order meets the highest standards in manufacturing and is constructed with safe, durable material.
Total Factory Building Area Across 4 State-of-the-Art Plants
Annual Export Volume of Sports Equipment & Ball Games Worldwide
Years of Specialized Manufacturing & Global Supply Experience
In-House Testing & Strict Quality Compliance Audit Coverage
We are a sporting goods manufacturer from China with more than 20 years of experience. We mainly produce soccer ball, football, basketball, volleyball, rugby…and other sports equipments. As the major supplier to the industry, we have four factories of 35000 square meters factory building, we are a long-term and stable supplier to many famous sports brands and major supermarkets around the world, and we export more than 20 million pieces of various ball games and sporting goods every year.
The global sports infrastructure and heavy-duty industrial mesh market has experienced exponential growth, driven by rigorous safety standards, massive stadium developments, and expanding recreational facilities across North America, Europe, Asia-Pacific, and emerging economies. As a cornerstone of both competitive sports containment and industrial safety engineering, heavy-duty ball nets require exceptional tensile strength, UV stabilization, and impact absorption characteristics. Sourcing from premier Chinese manufacturing hubs enables global B2B buyers, stadium architects, and municipal distributors to secure industrial-grade products that meet international compliance without compromising cost-efficiency.
Market analysts note that procurement managers increasingly prioritize suppliers possessing integrated supply chains. By managing everything from raw polymer extrusion and high-tenacity multifilament twisting to automated knotless weaving and rigorous drop-testing, leading Chinese manufacturers deliver unmatched structural integrity. This vertically integrated model insulates global partners from volatile raw material fluctuations while ensuring stringent adherence to environmental and mechanical safety protocols.
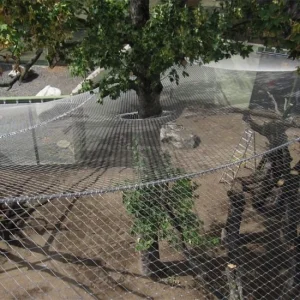
Heavy duty ball nets and professional sports containment systems serve multifaceted commercial applications, ranging from multi-sport complex backstops and golf driving range perimeters to specialized architectural animal enclosures and industrial drone testing arenas. Our enterprise provides tailored B2B solutions designed for:
Navigating global import regulations demands rigorous adherence to regional compliance standards. Our manufacturing operations maintain active certifications including ISO9001, BSCI, SMETA, CE, and CPSIA, ensuring full regulatory alignment for markets in the United States, the European Union, Australia, and beyond. We provide localized documentation, material safety data sheets (MSDS), and third-party lab testing reports (SGS, TUV) with every enterprise shipment.
To support localized deployment, our technical engineering team collaborates directly with regional contractors and distributors to provide customized structural wind-load calculations, anchor placement guides, and installation blueprints. This consultative approach minimizes deployment friction and guarantees long-term structural reliability under diverse climatic conditions—from sub-zero alpine environments to high-UV tropical installations.
The future of heavy-duty netting technology relies heavily on material science innovations and smart manufacturing integration. Our R&D roadmap focuses on several transformative breakthroughs:
Explore our diverse portfolio of professional balls, protective gear, training accessories, and custom athletic wear.
Professional insights into manufacturing capabilities, material selection, and global B2B procurement.
For demanding outdoor environments, high-density polyethylene (HDPE) treated with advanced UV inhibitors and high-tenacity nylon (polyamide) are the industry standards. HDPE offers superior moisture resistance and chemical inertness, while nylon provides exceptional tensile elasticity and breaking strength under high-velocity impact.
Yes. With over 35,000 square meters of factory floor space and dedicated in-house design and prototyping teams, we specialize in fully customized OEM/ODM orders. We can tailor mesh aperture sizes, twine thicknesses, perimeter border ropes, and corporate logo integrations to meet exact project blueprints within a 3-day turnaround for samples.
Our operations strictly comply with global manufacturing benchmarks. We hold certifications including ISO9001 for quality management, BSCI and SMETA for social compliance, as well as CE and CPSIA safety approvals, ensuring seamless customs clearance and compliance across North American and European markets.
Standard production lead times range from 15 to 25 days depending on the scale of the order. Through strategic partnerships with leading global logistics providers and direct carrier agreements, we ensure optimized freight costs and reliable door-to-door delivery worldwide.
 Insider Sports